- All
- Product Management
- News
- Introduction
- Enterprise outlets
- FAQ
- Enterprise Video
- Enterprise Atlas


Contact Us
5D Yaohai Urban Industrial Park, Yaohai District, Hefei City, Anhui Province
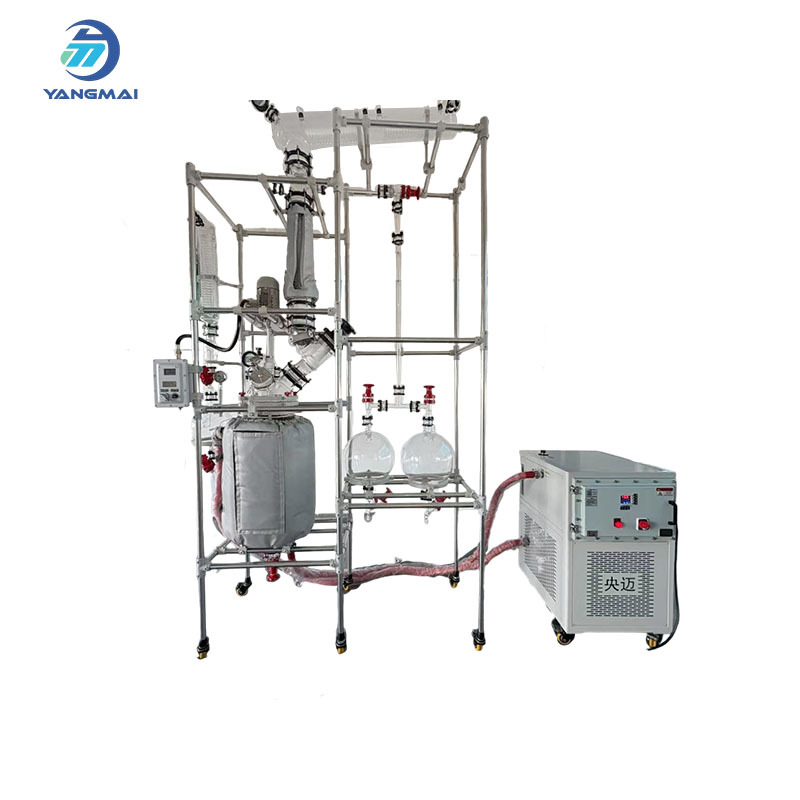
100L Explosion-proof Glass Distillation Reactor
Products include: chemical glass pipeline equipment; Glass condenser; Complete set of glass reactor; High temperature, low temperature and high and low temperature integrated machine temperature control equipment
Product Classification:
Key words:
Product Description
The 100L glass distillation reactor is engineered from high borosilicate glass, offering exceptional transparency, chemical resistance, and durability. Designed for solvent recovery, purification, and compound separation, it delivers reliable performance in pharmaceutical development, fine chemical production, and academic laboratories. With precise temperature control and compatibility with vacuum systems, this reactor ensures efficient distillation, crystallization, and reflux operations at laboratory and pilot plant scale.
2. High Borosilicate Glass Body – Provides excellent chemical resistance, durability, and clear visibility of reactions.
3. Advanced Distillation Column – Optimized for efficient vapor-liquid separation, solvent recovery, and product purification.
4. Vacuum Compatibility – Supports negative pressure operations, minimizing boiling points and improving distillation efficiency.
5. Temperature Control Flexibility – Compatible with heating and cooling circulators, allowing wide thermal operation ranges.
6. Corrosion-Resistant Sealing – PTFE and mechanical seals prevent leaks and ensure safe long-term operation.
7. Modular Configuration – Easily integrates with condensers, receivers, and pumps for customized process setups.
8. Industrial and Laboratory Use – Ideal for pharmaceutical research, chemical processing, and educational institutions.
Related Products
Message
Address: 5D Yaohai City Industrial Park, Yaohai District, Hefei City, Anhui China
Whatsapp:+86 15665455996
Tel:+86 13053083981
E-mail:youngmanglassreactor@gmail.com
Zip Code: 230011

Tiktok